Choose a platinum-cured silicone hose that complies with 21 CFR 177.2600. Match it to your temperature, pressure, cleaning method, and food type.
Three non-negotiables guide your selection: material compliance, performance ratings, and verifiable documentation. Look for FDA, NSF, and USP Class VI support. This guide helps you specify the right Silicone Hose with confidence.
Use platinum-cured silicone hose that meets FDA 21 CFR 177.2600 for safe food contact.
Match the hose to your food type, temperature, pressure, and cleaning method.
Request certificates of compliance and lot traceability to protect your product.
This regulation lists approved raw materials for rubber articles used in repeated food contact. Compliance for your Silicone Hose means every ingredient appears on that white list. The rule also sets extractables limits — 20 mg/in² for aqueous foods after seven hours and 175 mg/in² for fatty foods tested with n-hexane.
These limits differ from European food contact rules. Understanding both matters if you source equipment internationally.
|
Aspect |
FDA 21 CFR 177.2600 |
EU EC 1935/2004 |
|---|---|---|
|
Testing |
Extractables and migration |
Migration only |
|
Simulants |
Distilled water, n-hexane |
Water, acidic, alcoholic, fatty |
|
Limits |
20 mg/in² (aqueous), 175 mg/in² (fatty) |
Overall migration ~10 mg/kg |
|
Units |
mg per square inch |
mg per kg of food |
EU compliance does not automatically satisfy FDA requirements. Your hose must meet the limits for your specific food type.
Many buyers confuse "FDA-compliant" with "FDA-approved." The FDA does not approve finished food-contact articles. It approves individual substances through the Food Contact Notification process. Your hose can use FDA-listed resins but still fail if processing aids or pigments are non-compliant. Look for "FDA compliant under 21 CFR 177.2600" on documentation.
The FDA does not approve finished food-contact articles; it approves individual substances. A tube can be made from FDA-listed resins but still fail if processing aids or pigments are non-compliant. Look for 'FDA compliant under 21 CFR…' instead.
Common mistakes include treating all silicone products as interchangeable. Food-grade, medical-grade, and industrial silicone differ in purity and additives. Platinum-cured silicone offers higher purity than peroxide-cured versions. Do not assume 100% silicone is food grade. Fillers and cure byproducts can make a hose non-compliant.
One US sauce producer saved $1,200 buying no-name tubes online. Six months later, a health inspector found the tubes lacked FDA documentation. The producer destroyed $40,000 in finished product and paid a $25,000 fine. Always verify certificates of compliance and lot traceability.
Platinum-cured silicone uses a platinum catalyst for cross-linking. This clean chemistry route avoids organic peroxide curing agents. Fewer decomposition products remain in the finished material. You get very low extractables and leachables, excellent purity, and minimal odor or taste transfer. Peroxide-cured silicone can retain residual decomposition products such as acetophenone and benzoic acid derivatives. Post-curing may reduce these residues, but the curing chemistry leaves them inherently present.
|
Factor |
Platinum-Cured Silicone |
Peroxide-Cured Silicone |
|---|---|---|
|
Purity |
Ultra-clean, no by-products |
May leave residues |
|
Extractables |
Very low |
Higher risk |
|
Sterilization |
Withstands autoclave, gamma, CIP/SIP |
Degrades faster |
|
Applications |
Pharma, biopharma, cleanroom |
Industrial, non-critical |
This purity makes platinum cured silicone hose ideal for food, beverage, and medical applications. The material does not transfer taste or odor. USP <665> applies to silicone tubing contacting drug products. Aqueous extraction at pH 3, pH 7, and pH 10 at 40°C for 24 hours tests leachables. Organic extraction with 50% ethanol or isopropanol follows the same conditions. Analytical methods include GC-MS, LC-MS/MS, and ICP-MS. All compounds above the AET must be reported.
Silicone withstands a wider temperature range than PTFE, UHMWPE, and food-grade rubber compounds. PTFE handles high heat but offers less flexibility. UHMWPE provides excellent chemical resistance but limited thermal stability. Food-grade rubber compounds may crack or degrade under repeated cleaning cycles. Silicone remains flexible and durable across both hot and cold extremes.
You can specify FDA silicone hose for hot fill lines, CIP/SIP circuits, and cold beverage transfer. A food grade silicone tubing supplier should provide lot traceability and certificates of compliance. This durability reduces replacement frequency and downtime. The material resists aging and UV exposure better than many alternatives. Your Silicone Hose maintains performance through repeated sterilization without cracking or leaching.
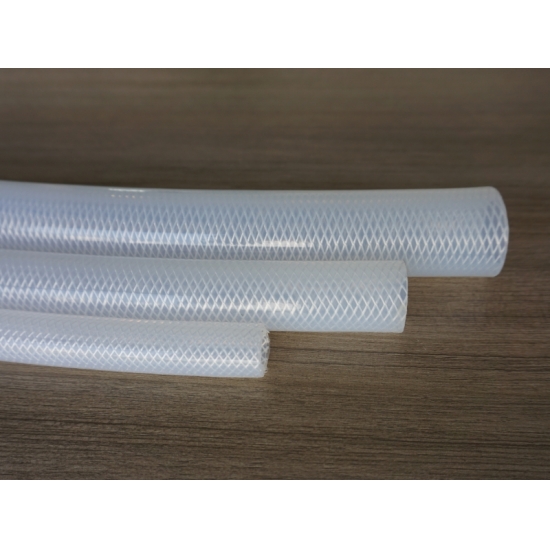
Start with the food itself. Fatty foods, acidic sauces, and alcoholic beverages attack hose materials differently. You need a FDA silicone hose rated for your specific product. Check the material certification first. A platinum cured silicone hose carries very low extractables, which protects delicate flavors.
Temperature range comes next. Silicone handles both hot fill lines and cold transfer, but you must confirm the rating for your process. A hose that meets your peak temperature with no margin will age faster. Pressure ratings matter just as much. Review the working pressure at your highest operating temperature, not at room temperature. Heat softens the tube wall and lowers burst resistance.
Size and thickness follow from flow rate and pressure drop. A thicker wall resists vacuum collapse and kinking. UV resistance matters for outdoor runs or skylit plants. Aging performance tells you how long the hose holds its properties under repeated cycles.
Cleaning method drives material choice. CIP and SIP cycles expose the tube to hot caustic, acid, and steam. These conditions cause most premature failures. Review the common root causes before you specify.
|
Root Cause Category |
Mechanism |
Resulting Failure Mode |
|---|---|---|
|
Improper installation or incorrect compression |
Sizing errors, misalignment, over- or under-compression, twisting, kinking, wrong groove fit |
Accelerated deformation, cracks, loss of elasticity, leakage |
|
Temperature cycling |
Continuous heating and cooling |
Unpredictable expansion and contraction, altered seal pressure, growing micro-gaps |
|
Chemical exposure (CIP detergents, alkaline cleaners, sanitizers) |
Repeated washdown cycles attack silicone surfaces |
Softening, swelling, surface tackiness, breakdown |
|
Steam and moisture saturation |
High-pressure steam affects crosslink stability |
Hardening, loss of rebound, micro-cracking |
|
Harsh environmental conditions |
Exposure beyond design limits during CIP/SIP and temperature swings |
Swelling, hardening, loss of sealing force, shorter service life |
Chemical compatibility extends beyond cleaning agents to the food product itself. Verify the hose against every fluid it touches. Flexibility keeps installation simple and reduces stress at fittings. A stiff hose twists and kinks, which shortens life. Transparency lets you inspect for residue, discoloration, or buildup without disassembly. Ask your food grade silicone tubing supplier for a wall-thickness and flexibility sample before you commit to a full order.
The inner tube contacts your product directly. A platinum cured silicone hose uses a platinum catalyst during cross-linking. This clean chemistry leaves very low extractables behind. The tube stays inert against fatty foods, acidic sauces, and hot beverages. You get no taste transfer and no odor pickup.
Reinforcement layers sit between the inner tube and outer cover. A woven braid does the mechanical work here.
A reinforced hose adds a woven layer between the inner liner and the outer cover. That braid is usually nylon, polyester, aramid, or steel wire. It resists burst pressure, stops ballooning, supports the tube under vacuum, and prevents kinking.
The outer cover protects against abrasion, UV exposure, and chemical splash. It also carries printed identification for lot traceability.
|
Tubing Type |
Burst Pressure / Pressure Resistance |
Additional Effects of Reinforcement |
|---|---|---|
|
Reinforced silicone tubing |
Dramatically increased burst pressure and working pressure ratings |
Allows larger bore sizes without collapse under vacuum; adds abrasion resistance |
|
Unreinforced silicone tubing |
Relatively low burst pressure compared to PVC braided hose or polyurethane tubing |
Limited to lower-pressure applications |
For pneumatic applications above 4 to 6 bar, specify reinforced silicone with polyester or stainless braid.
Tri-clamp fittings dominate sanitary service. You tighten a clamp around two flanged ends for a smooth, crevice-free joint. This connection disassembles quickly for cleaning and inspection. Cam-lock couplings suit faster changeovers on transfer lines. Barbed fittings work for lower-pressure runs where you push the hose onto a nipple and secure it with a clamp. Match your fitting material to the product and cleaning chemicals. Stainless steel 316L remains the standard for food contact.
FDA compliance alone does not satisfy every buyer. Pharmaceutical, biotech, and dairy processors often demand USP Class VI certification alongside FDA and NSF listings. USP Class VI evaluates biocompatibility through three in vivo tests. Each test uses material extracts or implanted samples to detect adverse biological responses.
|
Required USP Class VI Test |
What It Evaluates |
|---|---|
|
Systemic Injection Test |
Acute systemic toxicity by injecting material extracts and observing harmful whole-body reactions |
|
Intracutaneous (Intradermal) Test |
Localized tissue irritation by injecting extracts beneath the skin and checking for redness, swelling, or inflammation |
|
Implantation Test |
Long-term tissue compatibility by implanting the material and monitoring for inflammation, necrosis, or adverse tissue response |
NSF certification adds another layer. NSF/ANSI 51 covers food equipment materials, and NSF/ANSI 61 addresses drinking water system components. A hose carrying both FDA and NSF marks gives you broader coverage across food and beverage lines.
Lot traceability ties every coil back to its production record. Ask whether each coil or assembly carries a lot number. Traceability helps you identify affected goods if a problem occurs after delivery. Without it, a single failed batch can force you to scrap your entire inventory.
A valid certificate of compliance should reference FDA 21 CFR 177.2600 or an equivalent standard. Request this document before you place any order. A formal Declaration of Compliance legally binds the manufacturer to their material claims. Pair it with complete batch traceability records.
Your food grade silicone tubing supplier should provide documentation covering every control point.
|
Control point |
Example record |
|---|---|
|
Raw material |
Supplier, compound code, and lot number |
|
Production |
Machine line, date, and operator record |
|
Dimensions |
Inside diameter, outside diameter, and length |
|
Pressure test |
Test pressure, duration, and result |
|
Appearance |
Surface, color, marks, and contamination check |
|
Packaging |
Quantity, label, and carton or pallet number |
Sunrise provides verifiable certificates of compliance and lot-level documentation to support audits and quality programs. This paperwork protects you during inspections and customer audits. Store certificates with your Silicone Hose lot records for the full service life. When a regulator or customer asks for proof, you can produce it within minutes instead of scrambling through emails.
Start by matching the reinforcement to your operating condition. The table below shows which construction fits each service:
|
Application Parameter |
Recommended Reinforcement |
|---|---|
|
Internal pressure / pulsating systems |
Braided or textile reinforcement |
|
Suction / vacuum / anti-collapse |
Wire reinforcement |
|
Frequent bending / flexing |
Reinforcement that supports shape without excessive stiffness |
|
High heat + tensile stability |
Fiberglass or aramid reinforcement |
|
Lightweight / compact assemblies |
Textile layers |
For pressure-focused systems, a braided reinforcement structure is often the better fit. For suction or anti-collapse performance, wire reinforcement may be more suitable. Each application demands a different build.
Beyond reinforcement, consider maximum operating temperature, the fluid being carried, and working pressure. Determine whether the hose sees vacuum. Evaluate vibration exposure, repeated flexing, and routing constraints. Color-coding each line by service helps your team identify hoses at a glance. Verify every parameter against your specific Silicone Hose before purchase.
Establish a regular inspection schedule. Check for blistering, delamination, and crazing before these defects cause failure. Blistering appears as bubbles or swelling on the outer cover. These indicate fluid migration through degraded inner layers. The hose structure is already compromised. Delamination means inner layers separate easily or show air pockets between them. Localized soft spots confirm the defect. Remove delaminated hoses from service immediately. Crazing shows as fine surface cracks visible when you flex the hose. Early rubber degradation from UV, ozone, or an inferior compound causes this condition. If cracks penetrate to the reinforcement layer, the hose becomes a critical defect requiring immediate removal.
Follow a clear urgency rule. Any single critical defect — leakage, bulging, cracking to reinforcement, or coupling movement — means remove from service immediately. Minor surface crazing not penetrating the reinforcement gets tagged and replaced within 30 days. Inspect fittings at the same interval. Loose or corroded fittings create leak paths. Keep records of every inspection and replacement. Lot-level documentation supports audits and protects your compliance program.
Confirm 21 CFR 177.2600 compliance, verify platinum curing, match temperature, pressure, and cleaning ratings, then collect FDA, NSF, and USP Class VI documentation. The cheapest Silicone Hose often fails inspection or shortens service life. Verified compliance delivers better long-term value. Consult Sunrise experts for application-specific recommendations and samples.
No. The FDA approves individual substances, not finished articles. Your FDA silicone hose is compliant when every ingredient appears on the 21 CFR 177.2600 list.
Specify a platinum cured silicone hose. Platinum curing leaves very low extractables and no taste or odor transfer. Peroxide-cured silicone may retain residues that compromise sensitive products.
Ask your food grade silicone tubing supplier for a certificate of compliance, USP Class VI support, NSF listings, and lot traceability records. These documents protect you during audits and inspections.
Sunrise Silicone Hose Co., Limited


Adresse : Suite 805, No. 341 Jiahe Road, Xiamen City, Fujian Province, China
E-mail : sales@siliconehose-china.com